Our Success Projects
At MR Space, we deliver racking and storage solutions tailored to your operational needs. Explore our completed projects across various industries to see how we bring storage requirements into practice.
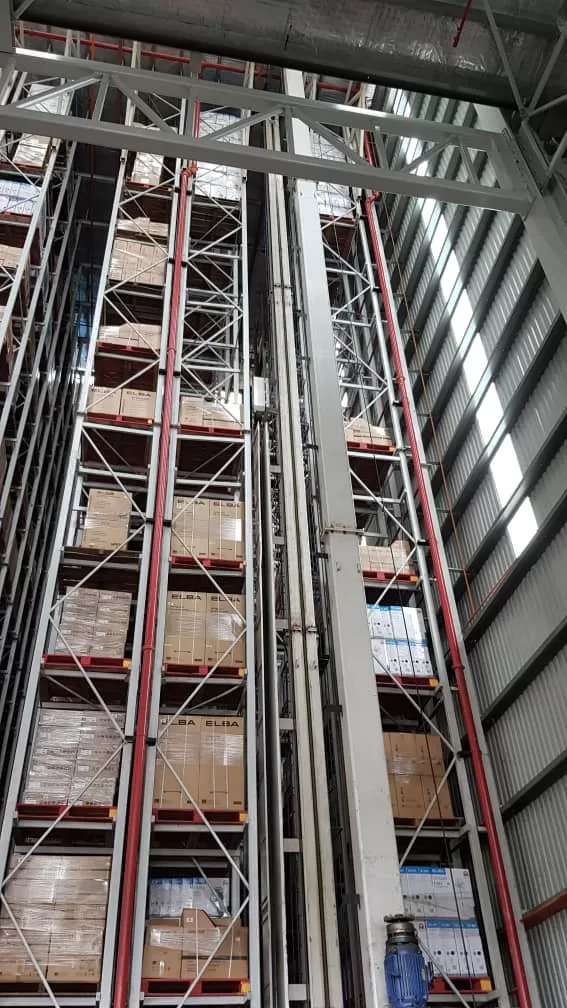
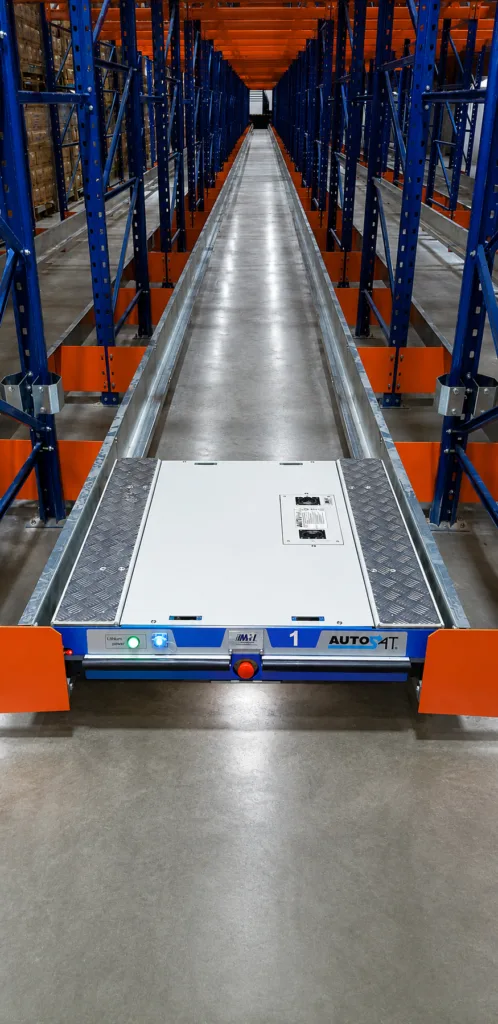
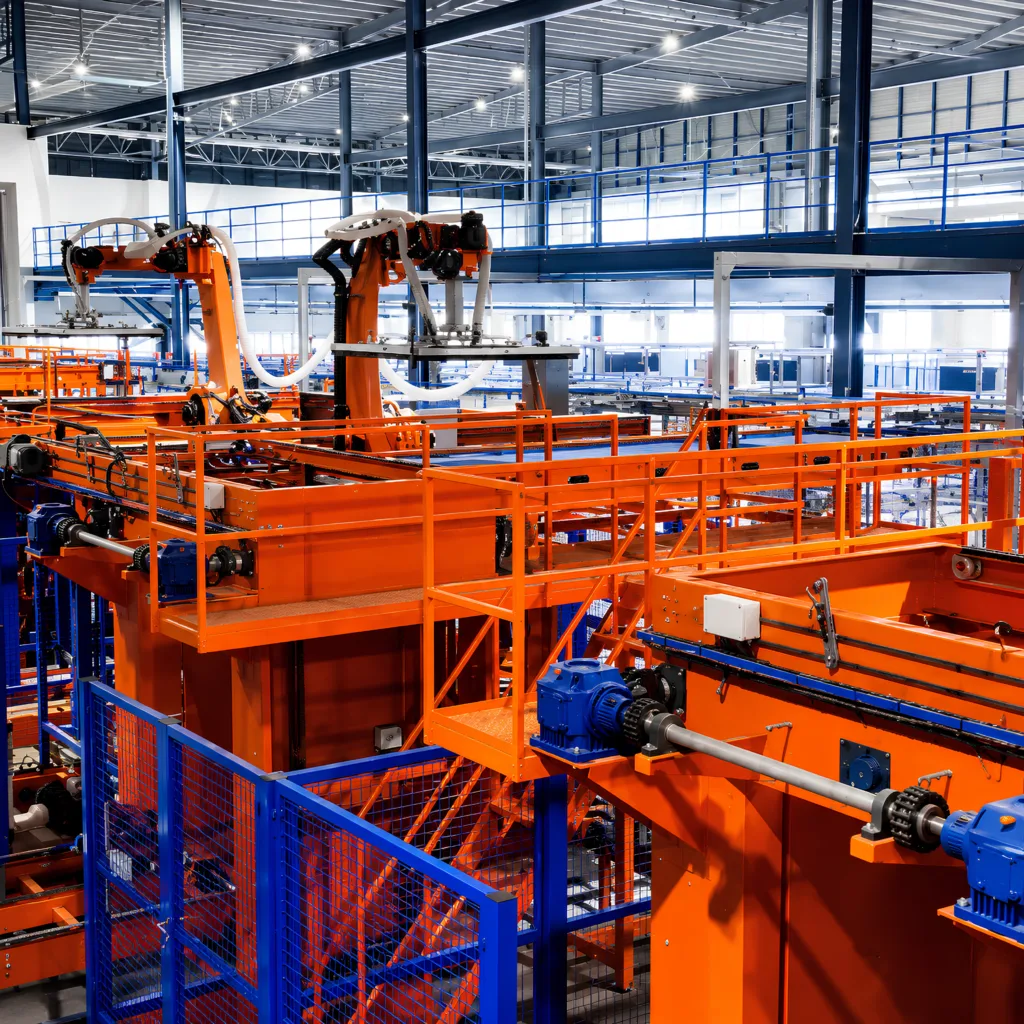
Automated Storage And Retrieval System Project
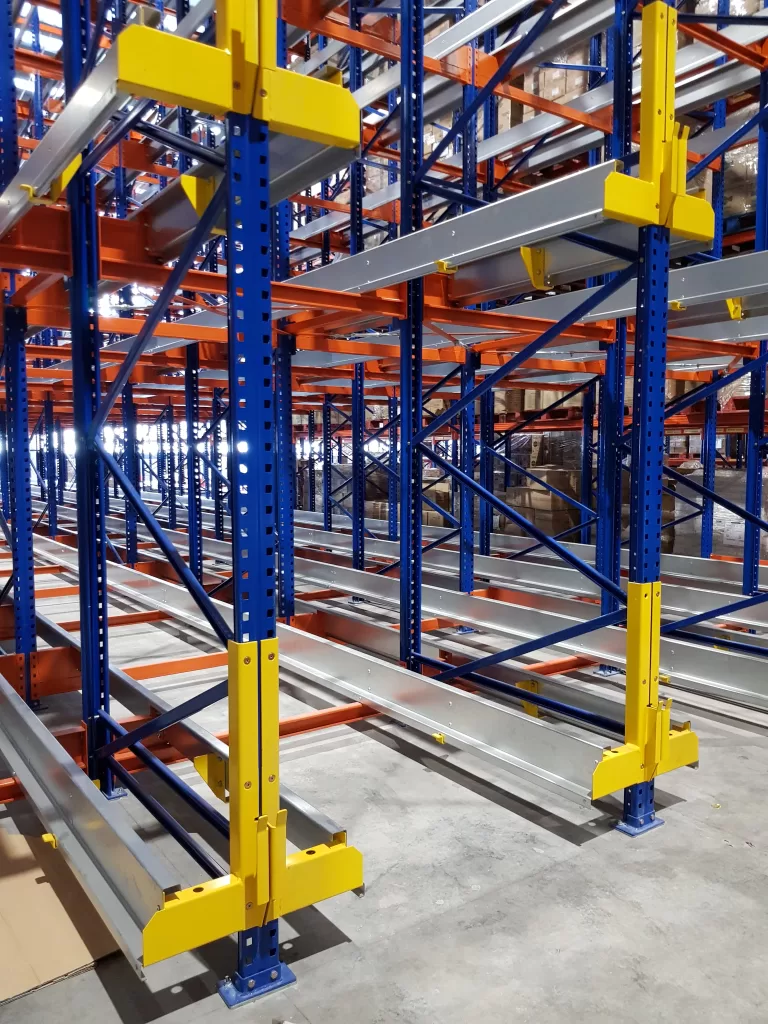
To meet the need for efficient warehouse storage and faster inventory handling, MR Space’s ASRS Racking System automates storage and retrieval operations while maximising vertical warehouse space. The system helps businesses optimise storage capacity, streamline workflows and improve warehouse operational efficiency.
Key Benefits
- Maximised Storage Capacity: Make better use of vertical space to accommodate more inventory within the available warehouse footprint.
- Automated Storage and Retrieval: Reduce reliance on manual handling by automating inventory movement.
- Improved Inventory Accuracy: Support more systematic stock tracking and inventory management.
- Enhanced Operational Efficiency: Streamline warehouse workflows and reduce time spent locating and retrieving goods.
- Reduced Manual Labour: Minimise repetitive storage and retrieval tasks to support more efficient resource allocation.
Looking to optimise your warehouse storage?
Explore MR Space’s ASRS Racking System to discover our automated storage solution and discuss your warehouse requirements with our team.


Mezzanine Floor Project
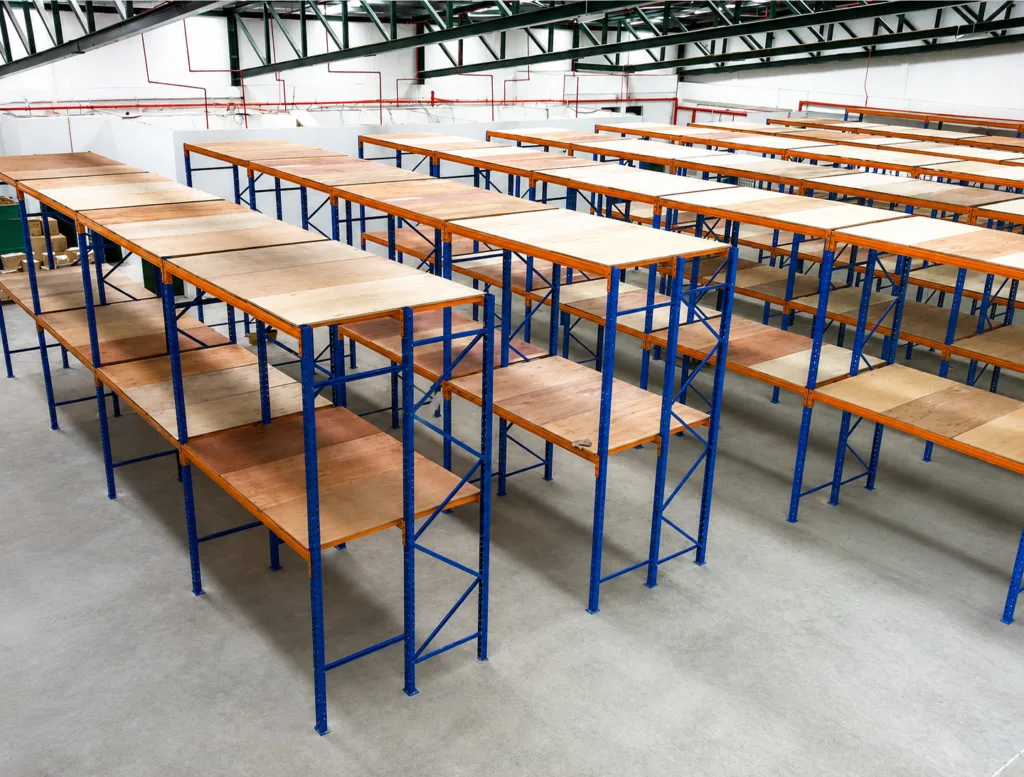
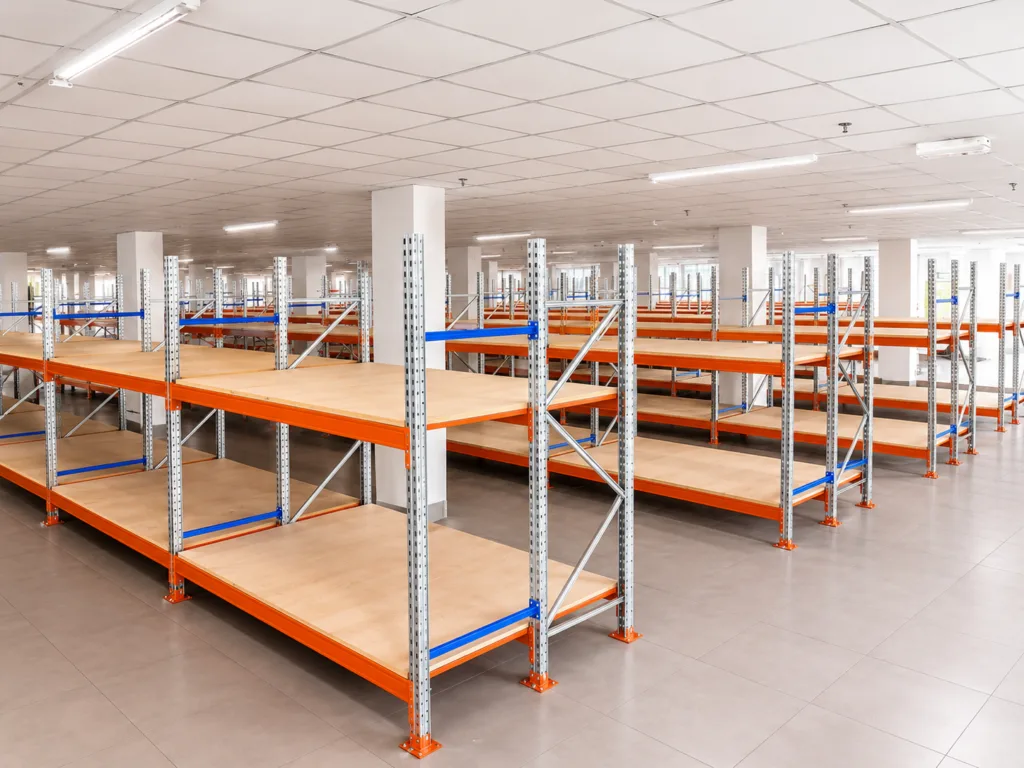
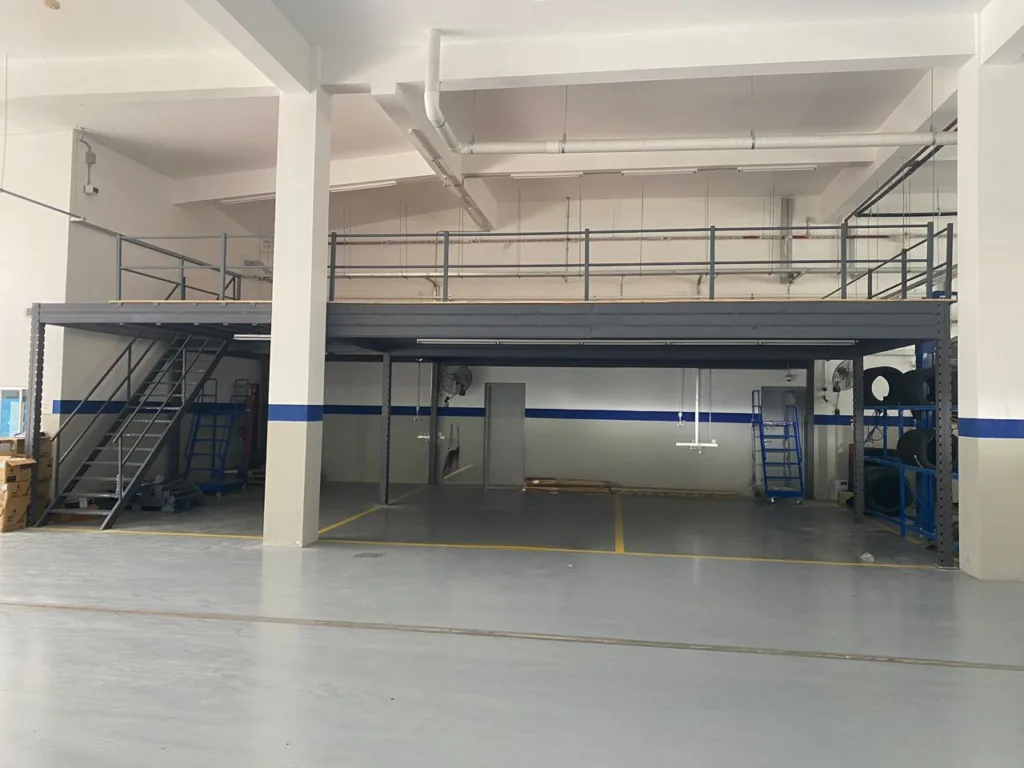
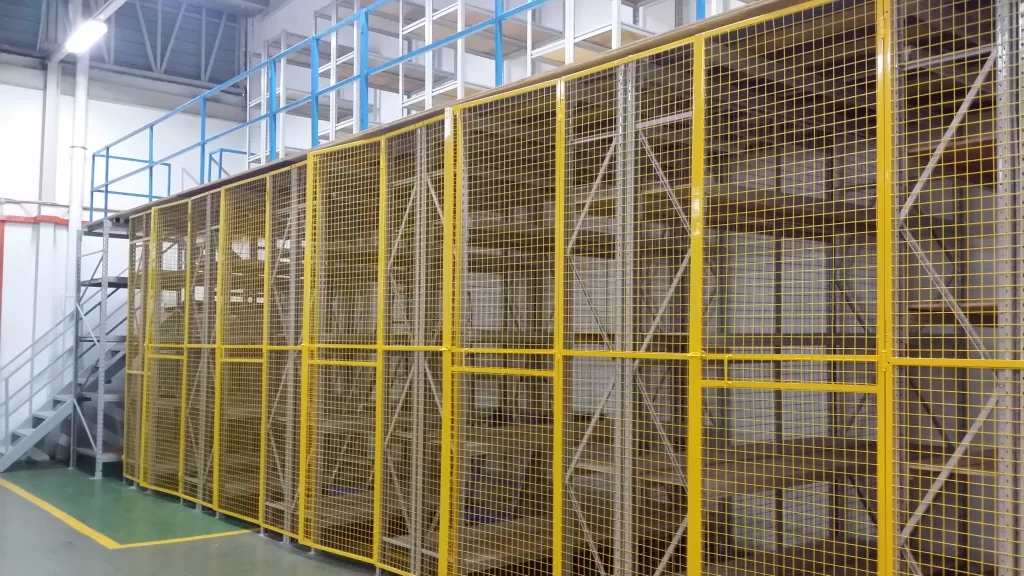
To maximise warehouse storage capacity while maintaining flexible ground-floor space, MR Space installed a mezzanine floor system that makes better use of the available vertical space. The system creates an additional usable level within the existing warehouse, providing more room for storage and other operational activities without expanding the building footprint. It is a practical solution for businesses looking to optimise warehouse space and improve storage efficiency.
Key Benefits
- Maximises vertical space utilisation without expanding the warehouse.
- Creates additional floor space for storage and warehouse operations.
- Keeps ground-floor areas available for inventory handling and daily activities.
- Supports different applications, including warehousing and office space.
- Offers layout flexibility to accommodate changing operational needs, depending on the system configuration.
Looking to maximise your warehouse space? Explore MR Space’s Mezzanine Floor Solutions to find a suitable system for your facility.


Selective Pallet Rack Project
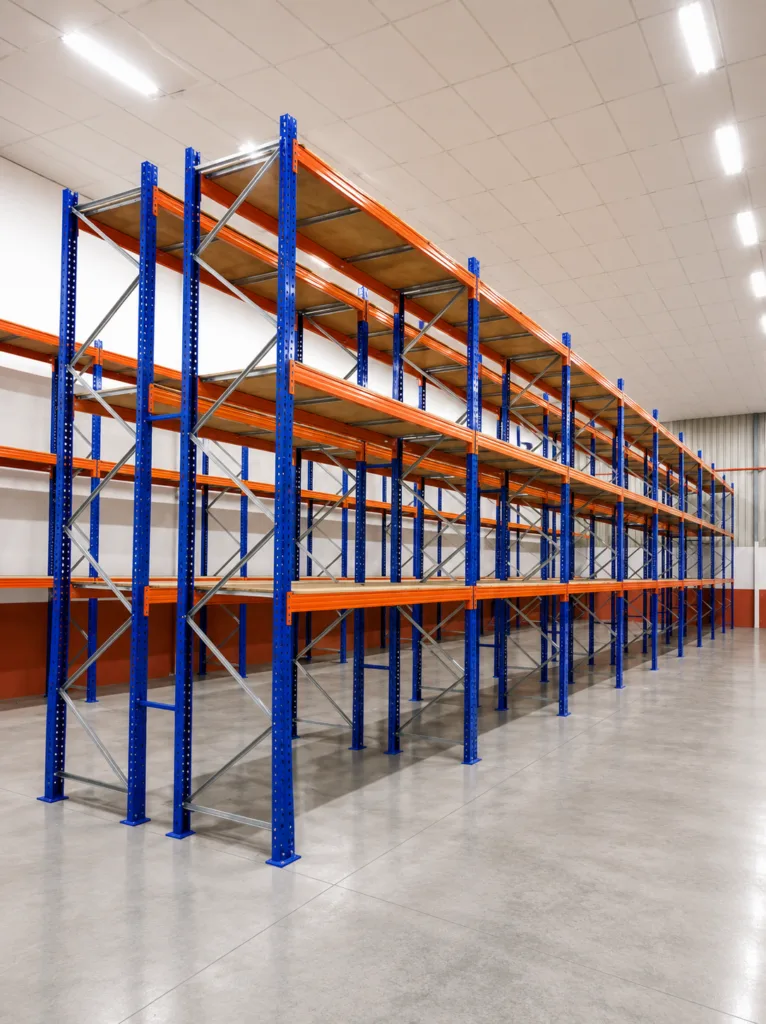
To improve warehouse storage capacity while maintaining easy access to individual pallets, MR Space installed a Selective Pallet Racking System tailored to the customer’s storage and operational needs. The system allows forklifts to access each pallet directly, making it suitable for warehouses handling different product types and requiring frequent stock movement.
Key Benefits
- Direct access to individual pallets for easier stock retrieval.
- Suitable for storing a wide variety of products and pallet sizes, subject to system specifications.
- Supports efficient inventory rotation and stock management.
- Makes effective use of available warehouse height.
- Offers flexible storage configurations to accommodate changing inventory requirements.
Looking for an efficient pallet storage solution? Explore MR Space’s Heavy Duty Racking Solutions for your warehouse.


Push Back Pallet Racking Project
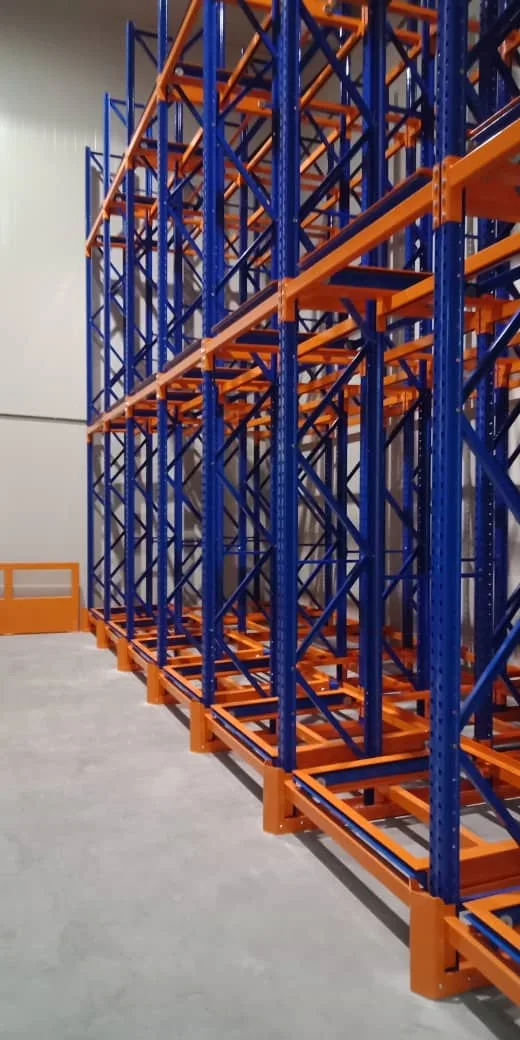
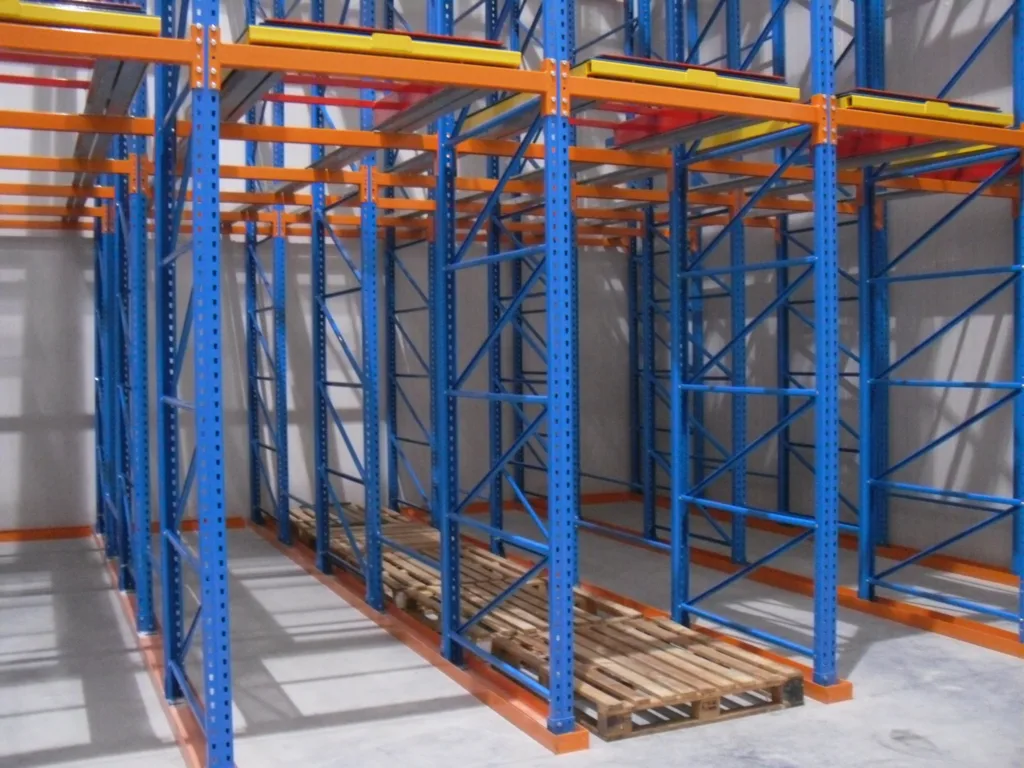
To increase pallet storage density and make better use of available warehouse space, MR Space installed a Push Back Pallet Racking System designed for storing multiple pallets at each storage lane. The system uses inclined rails and nested carts to allow pallets to be loaded and retrieved from the same aisle, reducing the need for a separate access aisle for every storage row.
Key Benefits
- Increases pallet storage density compared with conventional selective racking layouts.
- Reduces the number of aisles required for pallet storage.
- Allows multiple pallets to be stored in depth within each lane.
- Speeds up loading and retrieval by keeping pallet handling within the same aisle.
- Helps optimise warehouse space for operations handling multiple pallets of the same or similar products.
Need to maximise your warehouse storage capacity? Explore MR Space’s Heavy Duty Racking Solutions to find a suitable system for your storage requirements.

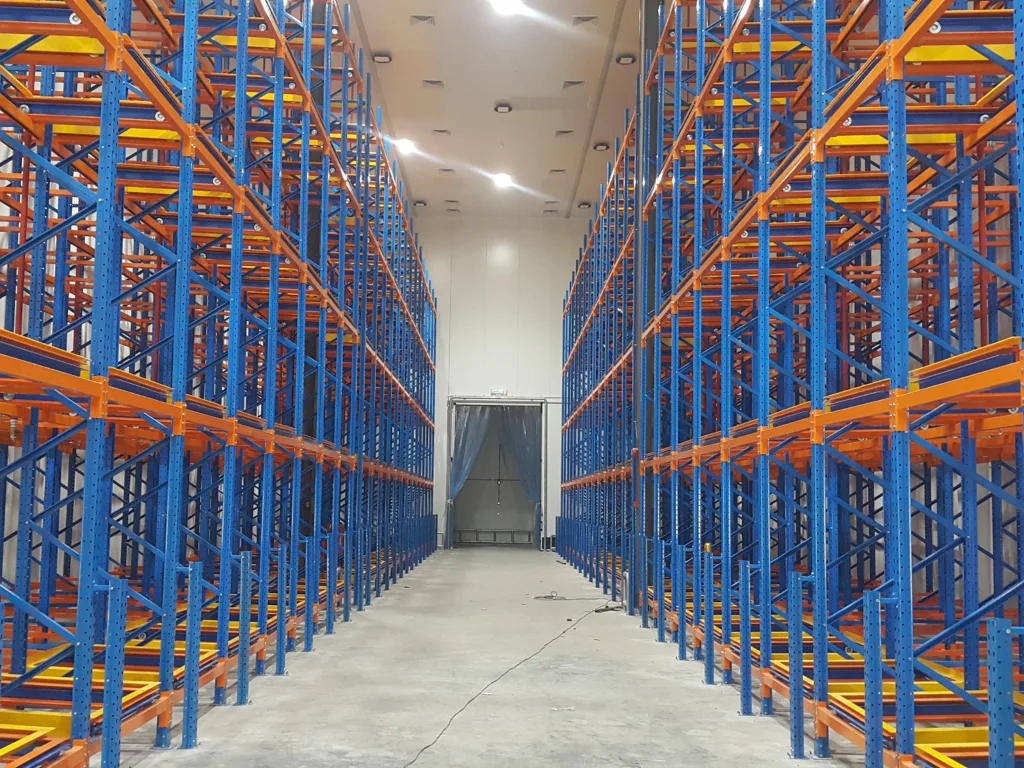
Twin Pallet Rack Project
To increase pallet storage capacity while reducing the space needed for individual storage aisles, MR Space installed a Twin Pallet Rack System that stores pallets two positions deep. This configuration helps businesses make better use of their warehouse floor space while maintaining access to pallet loads from the aisle. It is suitable for warehouses looking to balance higher storage density with practical inventory handling.
Key Benefits
- Increases pallet storage density compared with single-deep selective racking.
- Makes better use of available warehouse floor space.
- Reduces the number of aisles required for pallet storage.
- Accommodates higher volumes of palletised goods within the same warehouse footprint.
- Supports efficient warehouse storage when suitable forklift equipment and aisle access are available.
Looking to increase your warehouse storage capacity? Explore MR Space’s Heavy Duty Racking Solutions to find a suitable system for your warehouse.