Facility and EHS teams are being asked to do more with less: store more SKUs, speed up picking, reduce manual handling, and still keep workplace risk low. In that environment, racking and shelving decisions become safety decisions. The challenge is that “compliance” is rarely one single document or one single rule. It is a chain of choices—design assumptions, load ratings, anchoring, aisle widths, forklift interface, inspection routines, and change control—that must remain intact throughout the system’s life.
This article focuses on what facility teams in Malaysia should validate when specifying, buying, and operating an Industrial Shelving System Malaysia site teams can stand behind during audits and incident investigations. It does not attempt to quote or interpret any specific statute clause. Instead, it provides a practical compliance-and-safety checklist you can apply with your supplier, installer, and internal stakeholders—especially if you are upgrading an existing warehouse, adding a mezzanine, or standardising storage across multiple sites.
What “compliance” means for industrial shelving (and why it changes over time)
In practice, shelving and racking compliance is a combination of:
- Engineering integrity: The system must be designed for the intended loads, pallet types, and handling equipment, with correct beam levels, bay sizes, bracing, connectors, and anchoring.
- Site conditions: Floor quality, flatness, slab thickness, and the presence of drains, pits, joints, or ramps influence anchoring and stability.
- Operational controls: Safe loading discipline, forklift travel paths, impact protection, signage, and inspection routines must match the design assumptions.
- Documentation: As-built drawings, load notices, and inspection/maintenance records provide traceability. They are also what internal auditors and safety committees look for.
Why does compliance feel like it “updates”? Because your operation changes: new SKUs, different pallet footprints, heavier cartons, higher stacking, new MHE (material handling equipment), more throughput, or a new shift pattern. A shelving system that was “fine” for one use case can become unsafe when the use case changes without a formal review.
That’s why the most important update facility teams can make is not a product change—it’s a change-control mindset for storage systems. Whenever loads, layouts, or equipment change, you trigger a re-validation of the design and the safety controls.
Core safety elements to validate before you buy (specification checklist)
Procurement tends to compare capacity and price. EHS teams tend to ask about safety. Facilities tend to worry about installation time and floor conditions. A strong specification bridges all three.
Use the checklist below as a pre-purchase validation pack for any racking system or industrial shelving purchase, whether it is light duty, medium duty, or heavy duty storage.
1) Define the load case clearly (not just “kg per level”)
One of the most common failure points is a vague load definition. “1,000 kg per level” can mean very different things depending on how the load is distributed and what the pallet looks like.
- Unit load type: palletised goods, cartons, bins/totes, drums, long materials, or mixed.
- Load footprint: pallet size, overhang, or point loads from legs/skids.
- Load distribution: uniformly distributed load vs concentrated loads.
- Handling method: forklift, reach truck, stacker, hand pallet truck, or manual loading.
- Dynamic effects: impact and push forces from MHE, especially for high-traffic aisles.
Practical example: If operations change from standard pallets to non-standard skids, the contact points may shift to smaller areas. That can overload beams or decking even if the total weight stays the same. Build this risk into your specification by listing the exact unit load geometry and how it will be placed on each level.
2) Confirm frame, beam, and connector details (not only the brochure model)
When comparing suppliers, insist on engineering-relevant details and ensure the offer matches the final as-built system:
- Upright/profile type and thickness; beam section and connector type
- Bracing configuration and bay length
- Beam locking mechanisms and safety pins
- Decking type (if used), fixing method, and load suitability
- Accessories that affect safety: pallet supports, backstops, row spacers, tie beams
For medium duty shelving (e.g., longspan) that is manually loaded, validate shelf panel type and how deflection is managed over time. For heavy duty pallet racking, validate impact resistance planning (upright protectors, end-of-aisle barriers) based on your forklift routes.
3) Floor and anchoring assumptions must be stated
Anchoring and base plate selection depend on the slab. Don’t accept “anchor as required” without confirming the basis of design.
- Confirm whether site measurement and floor assessment are included.
- Clarify anchor type and embedment assumptions, especially near joints or edges.
- Require the installer to highlight any floor issues that must be repaired before installation.
Practical example: A warehouse may have a high-quality slab in the main storage area but a thinner slab near loading bays or older extensions. If the heaviest bays are installed in the weakest zone, the system can become vulnerable even if the racking itself is correctly manufactured.
4) Operational geometry: aisles, clearances, and picking ergonomics
“Compliant” storage is also storage people can use without taking shortcuts. Validate:
- Aisle widths suitable for the actual MHE turning radius and load length
- Clearances to sprinklers, lighting, ventilation, and emergency routes
- Safe access for picking: step platforms, pick modules, or dedicated pick faces
- Guarding and segregation between pedestrians and MHE paths
These points often determine whether your operation will keep to the designed load positions and whether impacts will be frequent. When impacts are frequent, inspections and protection become more critical.
Documentation and traceability facility teams should request (and keep updated)
Documentation is not “extra”—it is part of the safety system. During audits, incident reviews, or site handovers, the ability to show what was installed and what loads it was designed for is essential.
Request a minimum documentation set and store it in a controlled location accessible to EHS and facilities:
- Layout and elevation drawings: showing bay counts, beam elevations, and aisle design.
- Load notices: clear guidance on maximum loads per level/bay and any placement rules.
- Installation method statement: including anchoring approach and torque/fastener checks where applicable.
- As-built confirmation: record of any deviations from the initial design and approvals for changes.
- Inspection and maintenance plan: what to check, how often, and what triggers immediate action.
If your organisation has multiple facilities, standardise the template for load signage and inspection logs. Consistency makes it easier to audit and reduces confusion for transferred staff.
For readers comparing solutions, this is also a good time to review broader storage system options and how they affect operations. See The Advantages Of Industrial Storage Systems for a structured overview of common approaches and where they fit.
Inspection and maintenance updates: what “good” looks like on the warehouse floor
Even a well-designed system becomes unsafe without consistent inspections. The most useful update you can implement is a clear internal standard for inspections with defined escalation rules.
Set a tiered inspection routine
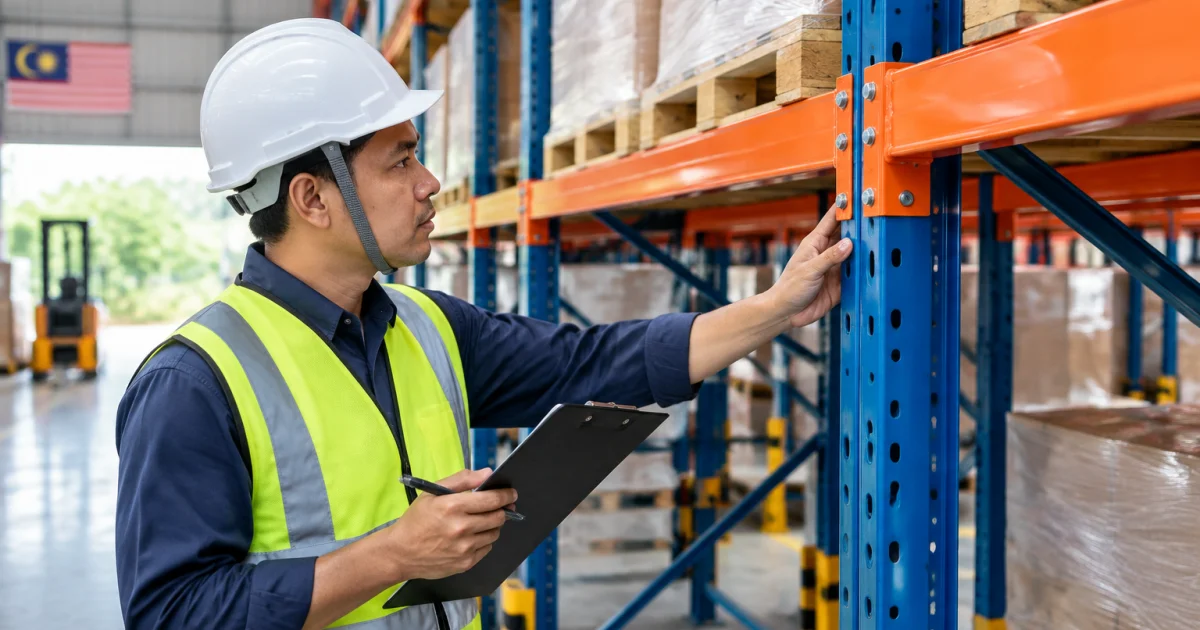
- Daily/shift checks (operational): quick visual scan by supervisors or forklift leads—look for obvious impacts, displaced pallets, missing pins, loose decking, or blocked aisles.
- Monthly checks (facility): structured walk-through with a checklist and photos, verifying upright damage, beam deflection, anchor condition, and safety accessories.
- Periodic expert review: deeper assessment, especially after layout changes, new equipment, or repeated impacts in a zone.
The key is not the frequency alone; it’s the trigger conditions for action. Define what requires: (1) monitor, (2) unload and isolate the bay, or (3) immediate shutdown of an aisle pending evaluation.
Common non-compliances found in real facilities (and how to prevent them)
- Overloading by “temporary” staging: solved by providing a dedicated staging lane or floor-marked buffer area.
- Mixed pallet quality: broken or non-standard pallets increase beam damage and collapse risk; implement pallet acceptance rules.
- Missing or bypassed locking devices: keep spare safety pins/locks and treat missing locks as a stop-work issue for that bay.
- Unreported forklift impacts: install end-of-aisle protection and create a no-blame reporting channel tied to quick repairs.
- Ad-hoc modifications: relocating beams, adding levels, or cutting braces without engineering review; enforce change control and tag affected bays.
These issues appear across warehouse storage Malaysia sites regardless of industry, because they are driven by pressure for throughput. Preventive design (good layout and protection) plus disciplined inspections is the most cost-effective approach.
Layout changes, expansions, and mezzanine floors: where compliance risk spikes
Many facilities in Malaysia expand capacity without expanding footprint. Two common moves are (1) increasing storage height and (2) adding a mezzanine floor. Both can be safe and efficient when engineered correctly—but they raise the stakes for design integration and documentation.
When you reconfigure racking, treat it as an engineering change
Common “small” changes that deserve formal review:
- Changing beam elevations to fit new cartons or pallets
- Extending a row, adding bays, or switching from selective to higher-density configurations
- Changing forklift type (e.g., counterbalance to reach truck) which changes impact patterns and aisle needs
- Adding conveyors or pick modules that change access routes
Practical example: A facility increases beam height to add one more level. The total pallet count goes up, but so does the centre of gravity and the chance of contact with sprinklers or lighting. Without revalidation, the change can introduce both structural and fire-safety conflicts.
Mezzanine floor projects: integrate storage, people flow, and loading rules
Mezzanines are often requested to create extra space for picking, packing, offices, or light storage. The compliance mindset here is to treat the mezzanine as a system: structure, stairs, gates, barriers, and load management.
- Define intended use: storage only, work area, or mixed use.
- Set load limits and ensure signage is visible at access points.
- Control pallet transfer (e.g., via loading gates) to prevent falls.
- Plan emergency egress routes and keep walkways clear.
If you’re evaluating this option, read Custom Mezzanine Floor Solutions For Selangor Warehouses And Offices to understand how mezzanine planning ties into real warehouse constraints like vertical clearances and workflow.
How to evaluate suppliers and installers (questions procurement should add)
For BOFU buyers, supplier selection is where safety outcomes are determined. Two suppliers can offer similar-looking systems, but the difference shows up in engineering diligence, installation quality, and after-sales support.
Use these questions during quotation and technical evaluation:
Engineering and design
- Will you conduct a site measurement and confirm floor conditions before finalising drawings?
- What assumptions are you using for unit load, beam spacing, and handling method?
- How will you address impact protection for high-traffic aisles?
- Can you provide a layout that supports safe forklift travel paths and pedestrian segregation?
Installation controls
- Who supervises installation and what checks are performed before handover?
- How do you verify verticality/plumbness and correct beam engagement?
- What is your approach to anchoring near joints, edges, or uneven slabs?
Handover, training, and lifecycle support
- Do you provide load notices, as-built documentation, and a recommended inspection checklist?
- Can you support expansions or reconfigurations with updated drawings?
- What is the process for replacing damaged components and preventing incompatible substitutions?
This evaluation logic applies whether you’re sourcing a light/medium shelving line for parts storage or a heavy duty racking system for pallets. If your project is in a high-growth area such as Johor, the risk of rushed expansions is higher—so build these requirements into the purchase order scope rather than treating them as “nice-to-have”.
Choosing the right system type without creating new compliance gaps
Many teams start with the keyword “racking system” and then get lost in options. The safest path is to match the system to your inventory velocity, access needs, and handling method—then validate the compliance elements discussed earlier.
Selective pallet racking (common baseline)
Works well when you need direct access to many SKUs. Compliance focus: impact protection, clear load ratings, and aisle design for forklift turning and visibility.
High-density options (drive-in, push-back, gravity flow)
Used to increase storage density. Compliance focus: tighter tolerances, disciplined loading practices, and higher impact likelihood. These systems often require stronger operational controls and training because misuse is easier.
If you are comparing high-density solutions, it helps to benchmark how similar systems are built and supported. For instance, reviewing a product configuration like 6500 Series Heavy Push Back Pallet Racking System can clarify what components, guide rails, and safety elements are typically included—so your specification is not missing key items.
Longspan and modular shelving for cartons/parts
Often used for maintenance spares, e-commerce cartons, or assembly-line parts. Compliance focus: controlling shelf deflection, preventing climbing or over-stacking, and ensuring stability if units are tall or arranged in long runs.
Retail gondola and display shelving (backroom still matters)
For supermarkets and commercial outlets, customer-facing shelving gets attention, but backroom storage carries higher stacking and tighter aisles. Compliance focus: anchoring where appropriate, stable configurations, and avoiding ad-hoc add-ons. If you manage retail storage too, a reference point such as 80 Series Wall Island Gondola Shelving helps align display requirements with safe loading practices.
Implementation playbook: a step-by-step process facility teams can run
Below is an actionable workflow that reduces both procurement risk and operational risk. You can adapt it for any Racking System Malaysia project, from a small storeroom upgrade to a new distribution centre.
Step 1: Pre-design data pack
- Inventory profile: pallet sizes, max weights, carton dimensions, odd-shaped items
- Throughput: inbound/outbound patterns and peak constraints (qualitative is fine)
- MHE list: forklift types, mast heights, attachments, battery charging zones
- Building constraints: clear height, columns, doors, emergency exits, services
Step 2: Concept layout and risk review
- Validate aisles, travel paths, pedestrian segregation, and staging zones
- Identify high-impact zones and specify barriers/protectors
- Confirm where mezzanine floor solutions may reduce congestion or improve flow
Step 3: Technical specification and quotation comparison
- Compare offers on engineering assumptions, not just “capacity”
- Confirm included documentation and handover deliverables
- Require installer method and quality checks
Step 4: Installation, verification, and handover
- Check plumb, anchoring, beam locks, and accessories are installed as designed
- Install load signage and define storage rules with operations
- Train supervisors on what damage looks like and how to report it
Step 5: Operate, inspect, and control changes
- Run tiered inspections and keep records
- Review after any impact event or repeated damage pattern
- Use a formal change request for any reconfiguration
For teams that want more depth on how load ratings and safety verification tie together for pallet racking specifically, you may also find Choosing The Right Warehouse Racking System For Your Business Needs useful as a complementary selection guide.
Conclusion: turn “updates” into a repeatable compliance system
Local compliance and safety expectations for industrial shelving are best handled as a repeatable management system rather than a one-time purchase requirement. When facility teams clearly define load cases, validate floor and anchoring assumptions, demand traceable documentation, and enforce disciplined inspections and change control, shelving becomes a reliable asset—not a hidden risk.
If you are currently planning a new warehouse storage build-out, expanding capacity with a mezzanine, or standardising racking across sites, the fastest way to reduce uncertainty is to work with a partner that can design, manufacture, install, and support the system lifecycle with consistent documentation.
Frequently Asked Questions
What should be included in a compliance-ready industrial shelving specification?
At minimum: defined unit loads (weight and footprint), intended handling method (forklift/manual), bay and beam configuration, anchoring/floor assumptions, required protections (upright/end barriers), required documentation (layout, load notices, as-built), and an inspection/maintenance plan. A strong specification also states how changes (new SKUs, higher levels, different MHE) will be reviewed and approved.
How often should an industrial shelving or warehouse racking system be inspected?
Use a tiered approach: quick visual checks during daily operations, a structured monthly facility inspection with a checklist and photos, and a periodic expert review—especially after layout changes, repeated impacts, or introduction of new material handling equipment. The most important element is clear trigger rules for unloading and isolating damaged bays.
What are common safety non-compliances found in warehouse shelving and racking?
Common issues include overloading by temporary staging, mixed or damaged pallets, missing beam locks/safety pins, unreported forklift impacts, and unauthorised modifications such as moving beam levels or removing bracing. Prevent them with clear load signage, pallet acceptance rules, impact protection, reporting procedures, and formal change control.
When do mezzanine floor projects require extra compliance attention?
Whenever a mezzanine adds storage or work areas above ground level, you must define use and load limits, control pallet transfer with proper loading gates, maintain clear walkways and egress routes, and keep signage visible. Mezzanines should be treated as integrated systems—structure plus access, barriers, and operating rules—rather than just an added platform.
We need a heavy duty racking system in Johor—what should we verify with the supplier?
Verify that the supplier will perform site measurement and confirm floor conditions, provide a layout matching your forklift type and aisle needs, specify impact protection for high-traffic zones, deliver load notices and as-built documentation, and support inspections and future reconfiguration. Also confirm installation quality checks (plumbness, anchoring, beam engagement) before handover.
Need a compliance-ready shelving and racking layout for your facility?
Mr Space supports facility, EHS, and procurement teams with complete in-house storage solutions—from design and local manufacturing to professional installation and ongoing support. If you’re upgrading an industrial shelving line, planning a warehouse racking expansion, or evaluating a mezzanine floor to increase capacity, we can help you validate load cases, optimise layout flow, and document the system for safer operations.
Share your site constraints and inventory profile, and we’ll propose a storage solution that fits your workflow and safety expectations.


